Home
Core expertise
Stainless steelCarbon steelHastelloyPTFE liningMetalworkPipe bendingGeberit MapressGeberit Mepla
Industries
ChemicalPharmaFoodPetroleum and tank farms
Company
About usQualityCareersFrequently asked questionsContact
DEFRENIT
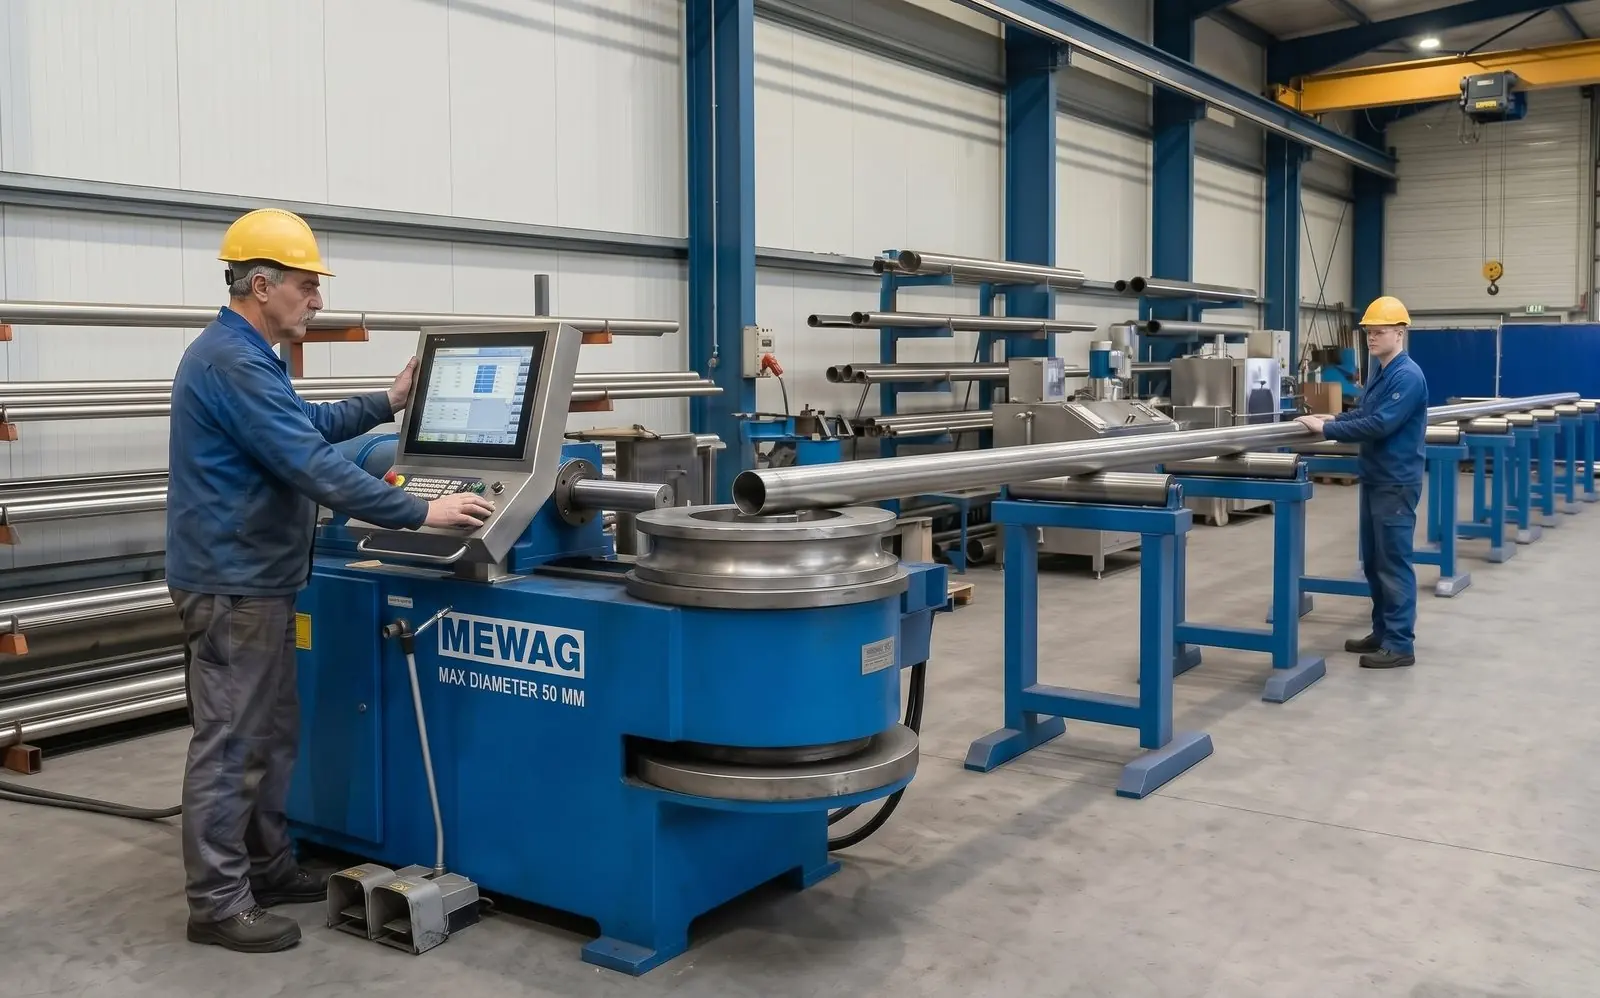
MEWAG hydraulic tube bending machine bending a stainless steel pipe

Pipe bending: bent pipes instead of welded elbows.

In our workshop in Pratteln we bend pipes from DN 10 to DN 50 on our two tube bending machines. Every bent elbow replaces two welds: fewer welds, less testing, a smooth inner surface.

Services · Pipe bending

When bending pays off

01

Many changes of direction

lines with many bends in a tight space, for example in plant rooms and around equipment.
02

Hygienic lines

every weld saved is one less point to inspect, pickle and document.

03

Small nominal sizes

instrument, control and utility lines from DN 10 to DN 50.

04

Short shutdowns

bent spools are prefabricated and installed faster.
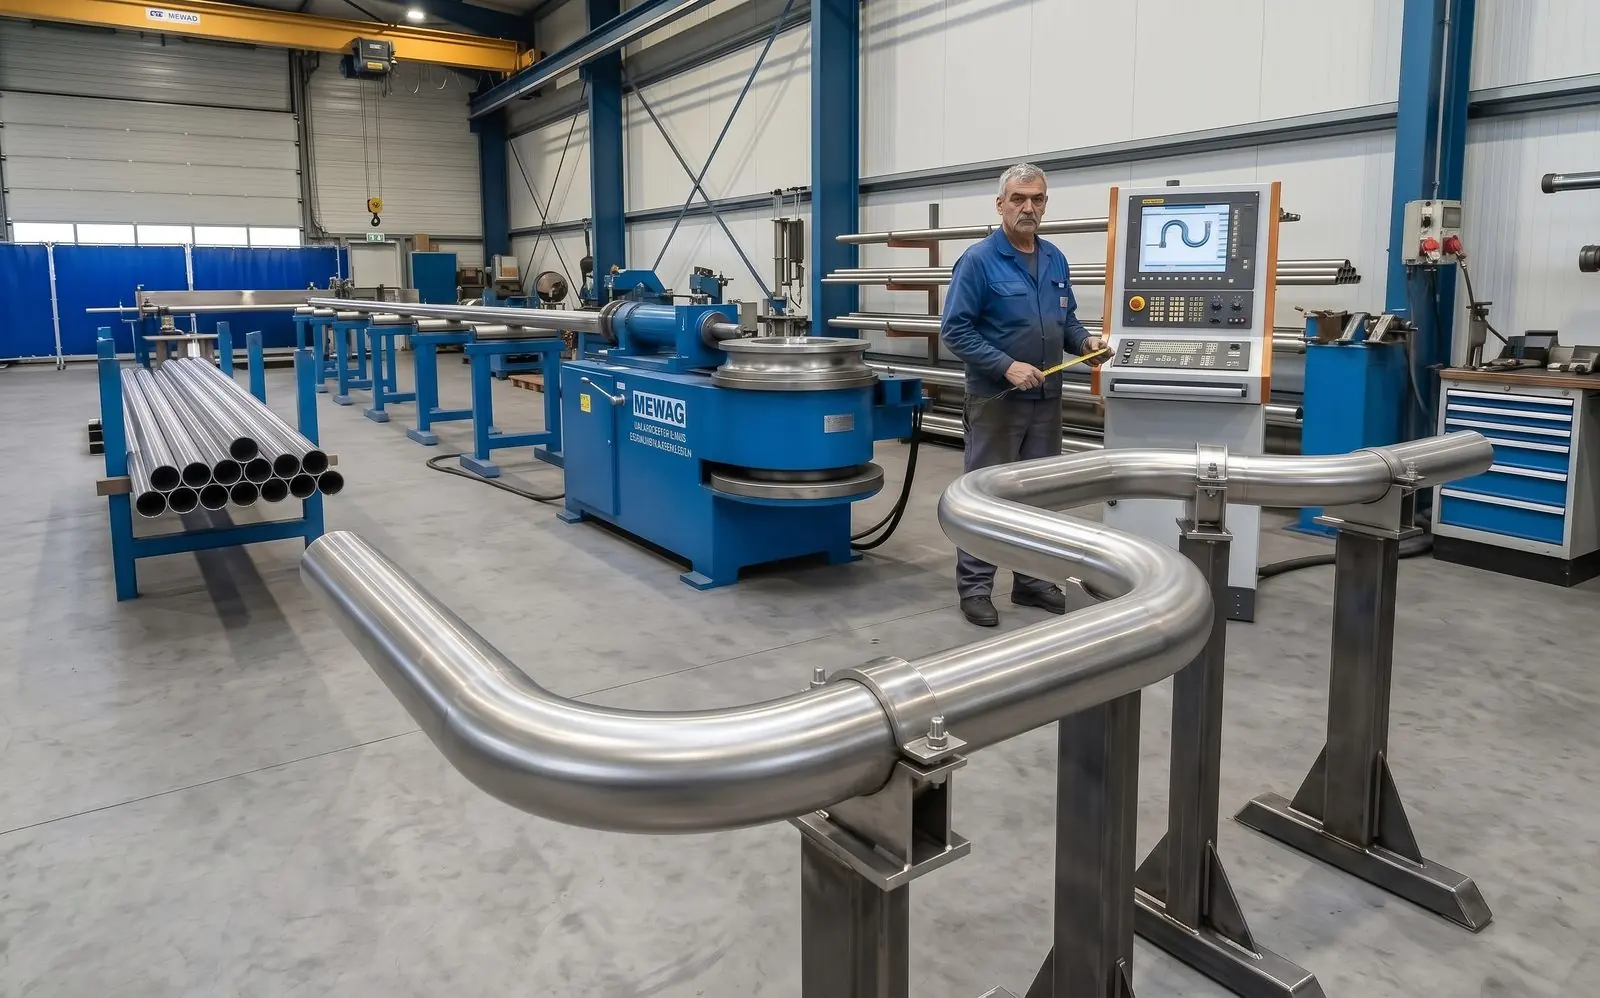
Bent stainless steel pipe on stands, with the tube bending machine in the background

Machines and bending range

Two tube bending machines stand in the workshop in Pratteln:

MachineBending range
MEWAG, hydraulicDN 15 to DN 50
ErcolinaDN 10 to DN 20

Which materials, wall thicknesses and bending radii are possible is clarified case by case from your isometric. Larger nominal sizes are made with welded elbows.

Why bend instead of weld

A welded elbow needs two welds, a bent pipe none. Every weld that is removed is one less possible point of failure.

  • Fewer welds — less testing, less documentation, less rework.
  • Smooth inner surface — no weld transition in the bend where product could settle.
  • Fewer fittings — elbows do not have to be purchased and stocked.
  • Shorter prefabrication — a spool with several changes of direction is made from one length of pipe.
Step by step

How we work

  1. Step 01

    Check the isometric

    we decide which bends are bent and which are welded.

  2. Step 02

    Bending in Pratteln

    on the Ercolina or the hydraulic MEWAG, depending on the nominal size.

  3. Step 03

    Inspection

    angles, dimensions and pipe cross-section on the bent piece.

  4. Step 04

    Welding and installation

    the spool is completed, tested and installed on your plant.

FAQ

Frequently asked questions

Up to what diameter can you bend pipes?

From DN 10 to DN 50. We use an Ercolina for DN 10 to DN 20 and a hydraulic MEWAG for DN 15 to DN 50. Larger nominal sizes are made with welded elbows.

Why are bent pipes better than welded elbows?

A welded elbow needs two welds, a bent pipe none. Fewer welds mean fewer possible points of failure, less testing and a smooth inner surface with no weld transition.

Which materials can you bend?

That depends on the material, wall thickness and bending radius. We check it from your isometric and tell you before quoting which bends can be bent.

Where are the pipes bent?

In our own workshop in Pratteln, as part of prefabrication. The bent spools are welded and tested there, then installed on your plant.
Contact

Let's talk about your project.

Hohenrainstrasse 10b, 4133 Pratteln · Mon–Fri 07:00–12:00 and 13:00–16:00